www.usa-automation.net
20
'26
Written on Modified on
PLC-Based Combustion Controls for Chemical Plant Boiler Systems
Nationwide Boiler integrates burner management, real-time SCADA visibility, and UL 508 panels to centralize industrial steam generation operations in demanding processing environments.
www.nationwideboiler.com
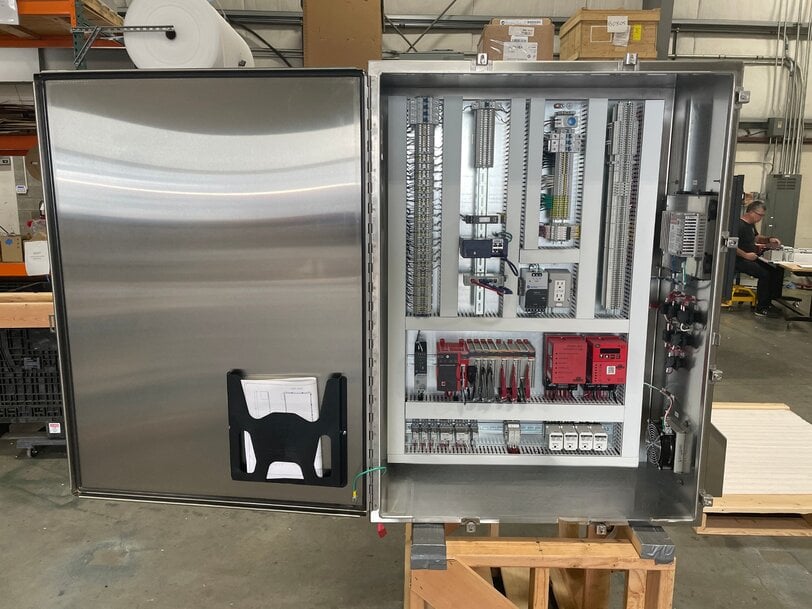
Nationwide Boiler Inc. has highlighted its PLC-based Combustion Controls, an integrated industrial combustion control and burner management system engineered for chemical manufacturing and processing facilities. Built on Allen-Bradley programmable logic controller (PLC) hardware, the system consolidates burner sequencing, firing control, and equipment diagnostics into a single UL 508-compliant architecture.
Centralized Industrial Combustion Control and Burner Management
Chemical processing plants rely on continuous steam generation where fluctuations in fuel-to-air ratios or burner trips can disrupt downstream reactors and heat exchangers. Rather than operating burner safety interlocks and firing-rate loops as isolated subsystems, Nationwide Boiler’s control packages coordinate combustion control and burner management functions through a unified Allen-Bradley PLC platform. This centralized architecture manages fuel and air delivery alongside burner startup, supervision, and shutdown sequences, supporting consistent thermal output across variable plant loads.
Custom HMI and SCADA Integration for Real-Time Monitoring
To connect boiler room equipment with broader plant automation networks, the system incorporates custom human-machine interface (HMI) and supervisory control and data acquisition (SCADA) configurations. Operators gain continuous visibility into individual equipment parameters, enabling real-time fault identification and operational adjustments. By surfacing equipment-level diagnostic data directly to control room personnel, the architecture helps maintenance teams reduce unplanned downtime and maintain safe operating margins for plant staff.
Standardized UL 508 Safety Compliance
Every control package is supplied with UL 508 listed control panels as standard. Compliance with the UL 508 standard for industrial control equipment verifies that panel wiring, component spacing, overcurrent protection, and enclosure ratings meet North American electrical safety requirements for industrial facilities. For chemical plant engineers, standardized panel certification simplifies regulatory audits and field inspections during commissioning or boiler control retrofits.
Additional Context
This section details technical specifications and competitive benchmarking not included in the original news release.
A comparable PLC-based boiler control platform is the Cleaver-Brooks Hawk 4000, which also utilizes an Allen-Bradley PLC platform and UL-listed control panels. The Hawk 4000 integrates combustion control—including parallel positioning, O2 trim, and variable-speed drive (VSD) blower control—with a separate Honeywell CB780E or Fireye CB120E burner management system to satisfy NFPA 85 separation requirements. It includes a 7-inch or 10-inch Allen-Bradley PanelView Plus touchscreen HMI (with 12-inch and 15-inch multi-touch options on newer configurations) and supports Modbus and EtherNet/IP communications for SCADA and building automation integration. While the Hawk 4000 is offered as a preprogrammed package tailored primarily to firetube and smaller watertube boilers, Nationwide Boiler’s custom-engineered Allen-Bradley control packages are configured specifically to match existing plant SCADA architectures and site-specific chemical processing requirements.
Edited by Aishwarya Mambet, Induportals Editor, with AI assistance.
www.nationwideboiler.com
